Halo Light
Engineered for endurance and performance across exterior events, construction sites, and dynamic facade installations.


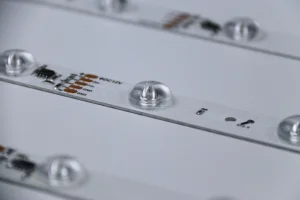
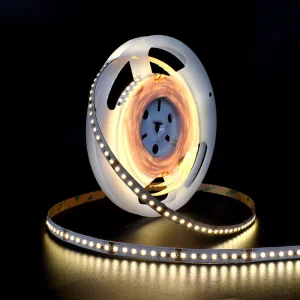
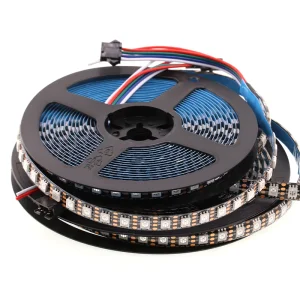

Why leading global distributors and EPC contractors choose China-engineered industrial lighting supply chains.
By controlling wafer binning, copper foil PCB design, automated SMT, and polymer extrusion within a unified industrial zone, we mitigate raw material inflation, maximize manufacturing yield, and provide consistent lead times for multi-kilometer infrastructure delivery.
Traditional PVC degrades rapidly under UV exposure. We leverage optical-grade food-contact silicone co-extrusion, delivering salt-spray endurance, IP68 immersion resistance, flame-retardant V-0 ratings, and anti-yellowing performance across temperature shifts from -40°C to +60°C.
Our dedicated laboratory runs integration sphere analysis, thermal cycling (-40°C to +85°C), salt spray, and pull-force tension testing. Every festoon batch complies strictly with CE, RoHS, UL 153, and ETL testing standards for North American and European imports.
Hangzhou Halo Light Co., Ltd. has steadily evolved into a competitive LED strip light manufacturer, specializing in advanced Neon Flex, SMD, and COB LED lighting solutions for global markets. Since its establishment, the company has focused on combining innovation, quality manufacturing, and customer-oriented service to meet the growing demand for energy-efficient and flexible lighting systems.
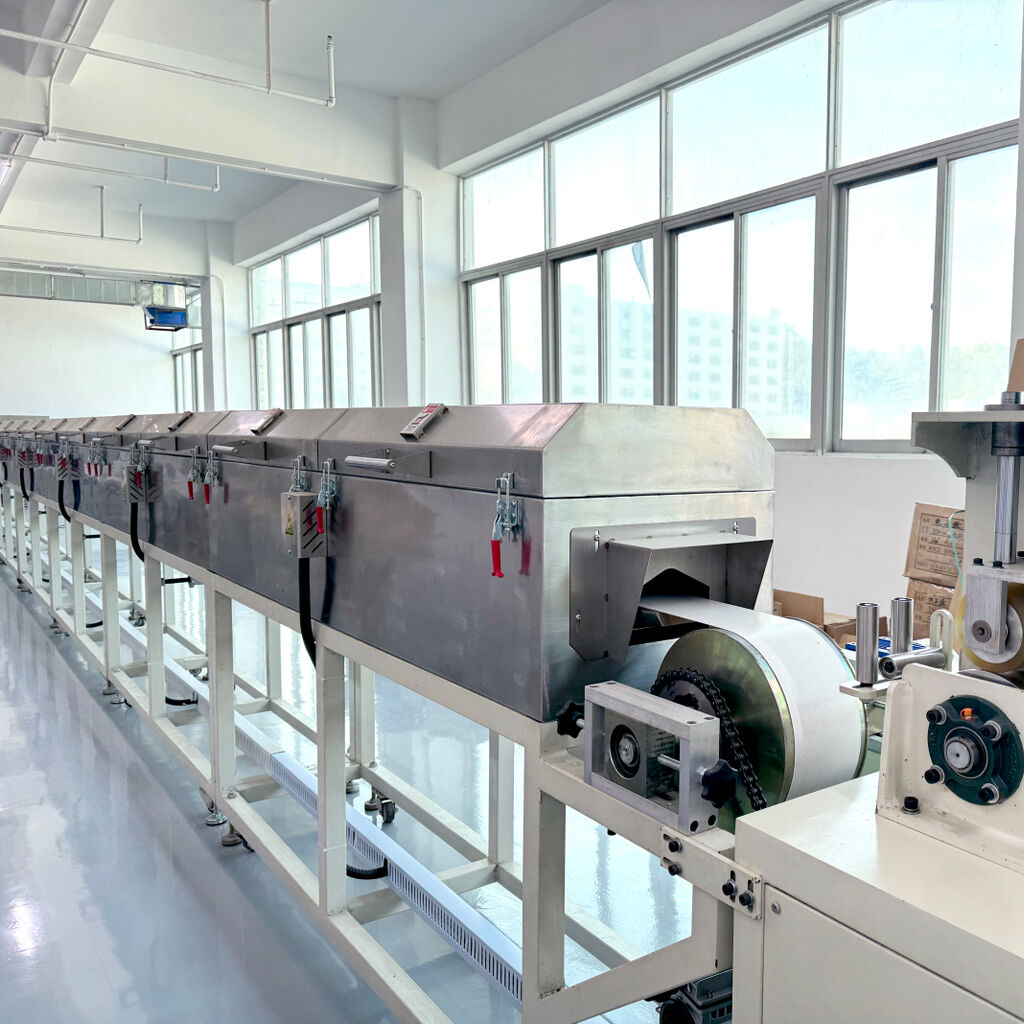
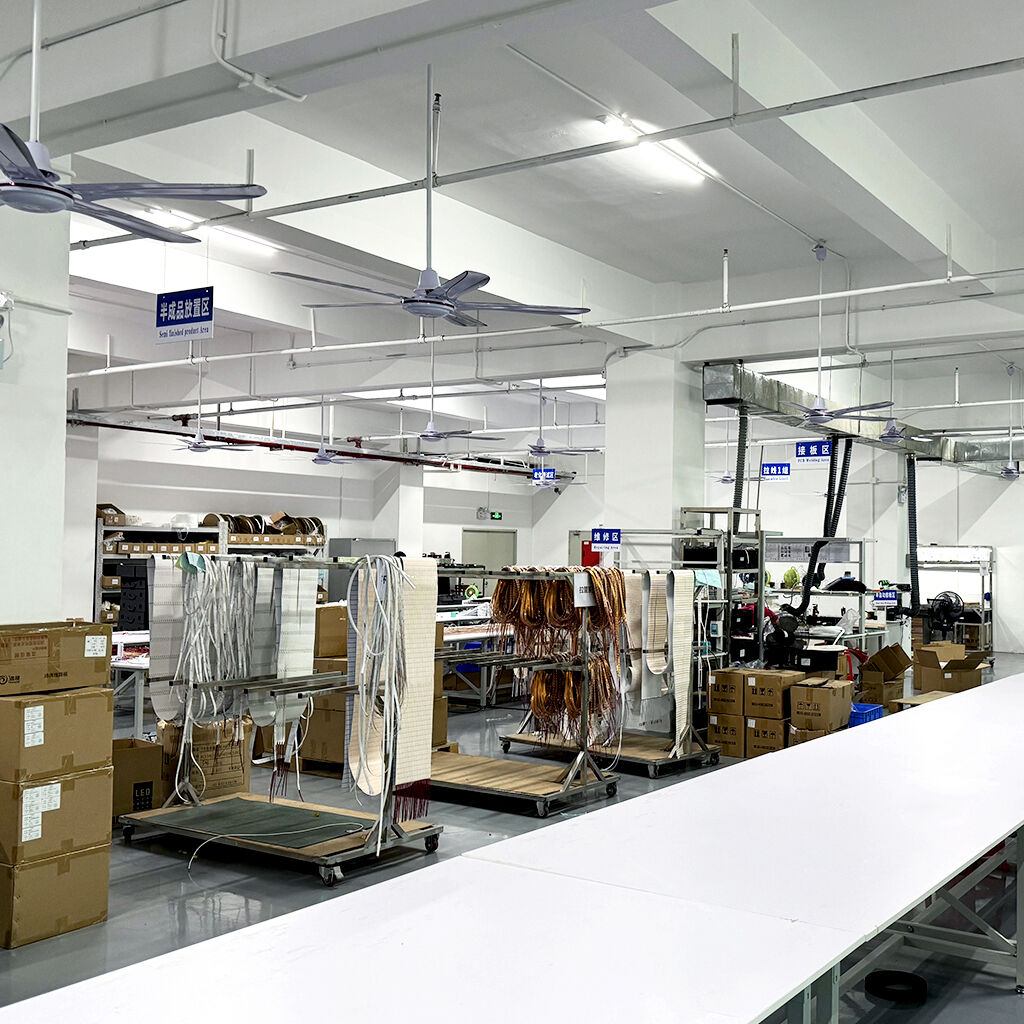
Based in Hangzhou, a key center for technology and manufacturing in China, Halo Light operates a modern production facility equipped with automated assembly lines and strict quality control processes. Over the years, the company has built a professional team of engineers and technicians dedicated to continuous product development and performance optimization.
With a strong emphasis on research and development, Hangzhou Halo Light has expanded its product range from standard LED strip lights to high-density COB strips, durable Neon Flex solutions, and intelligent lighting systems suitable for architectural, commercial, and residential applications. Its products are widely recognized for their stability, brightness consistency, and long service life.
Driven by global market trends and sustainable development goals, the company continues to enhance its manufacturing capabilities and expand its international presence, aiming to deliver reliable, efficient, and innovative LED lighting solutions worldwide.
The shift towards low-carbon infrastructure and intelligent lighting drives strategic upgrades across engineering sectors.
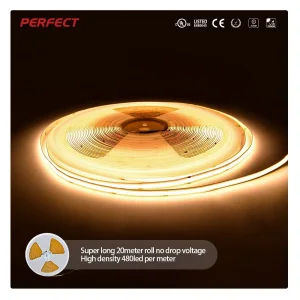
Eliminating lumen depreciation over 20-50m runs, integrated IC chips regulate DC current locally, ensuring identical lux levels across extensive continuous installations without voltage-drop issues.
The industry is transitioning from visible SMD spots to continuous phosphored Chip-on-Board (COB) architecture, delivering smooth diffuse light lines for architectural coves and exposed perimeter lines.
Modern festoon setups adopt DMX512, SPI Addressable protocols, Dali-2, and wireless mesh topologies, converting classic static illumination into responsive interactive canvases.
High-purity recyclable silicones replace PVC polymers. Optimized driver efficiency reduces total life-cycle carbon footprints in alignment with European Net-Zero mandates.
Engineered to excel in harsh external environments, commercial public venues, and intricate industrial setups.
Providing ambient overhead coverage across pedestrian boulevards, waterfront boardwalks, beer gardens, and resort verandas. Our IP68 siliconized systems withstand heavy rain, persistent solar radiation, and high coastal humidity without lens hazing or color drift.
High-voltage 220V driverless and low-voltage heavy-duty festoon setups provide continuous illumination across high-rise worksites, subway excavations, mine shafts, and modular scaffolding, featuring rupture-resistant cables and IP65/IP68 sealed sockets.
Addressing the demands of fast-paced rental staging, our high-flexibility festoon harnesses feature drop-resistant poly-carbonate caps, reinforced strain relief, and lockable waterproof connectors built for hundreds of assembly cycles.
Key technical parameters that electrical wholesalers, project contractors, and lighting designers must evaluate.
Verify PCB ounce weight (2oz-4oz pure copper) to prevent localized thermal bottlenecks that shorten diode lifespans and lead to color shifts.
For installations beyond 10 meters, specify constant-current designs or calculate precise secondary power feed dropouts across DC lines.
Prioritize food-grade silicone over conventional PVC to prevent micro-fracturing, yellowing, water ingress, and toxic outgassing over time.
Ensure suppliers provide verified third-party laboratory test reports for CE, RoHS, UL, and UKCA, preventing customs delays and regulatory fines.
Technical clarifications directly from our chief engineering and OEM procurement departments.
Silicone possesses exceptional molecular stability across temperature swings (-40°C to 200°C), total UV inertia, and resistance to coastal salt mist. PVC stiffens and cracks in cold conditions, discolors yellow under sun exposure, and deteriorates rapidly outdoors.
We deploy constant-current driver ICs on each strip cutting unit and select heavy-gauge 3oz/4oz dual-layer electrolytic copper PCBs. For extreme architectural distances, our 220V driverless linear festoons span up to 50–100 meters on a single feed.
We offer end-to-end customization: custom socket intervals, custom socket profiles (E27, B22, molded LED modules), specific CCT binning (±50K), private label cabling, sustainable packaging, and dynamic DMX512 or SPI programming.
Our production facilities operate under ISO9001:2015 frameworks. Our catalog is certified with CE-EMC, CE-LVD, RoHS, REACH, UL 153/2108, and ETL standards, enabling straightforward compliance and smooth customs clearance globally.
Complete your project specifications with precision-binned solid-state lighting hardware.